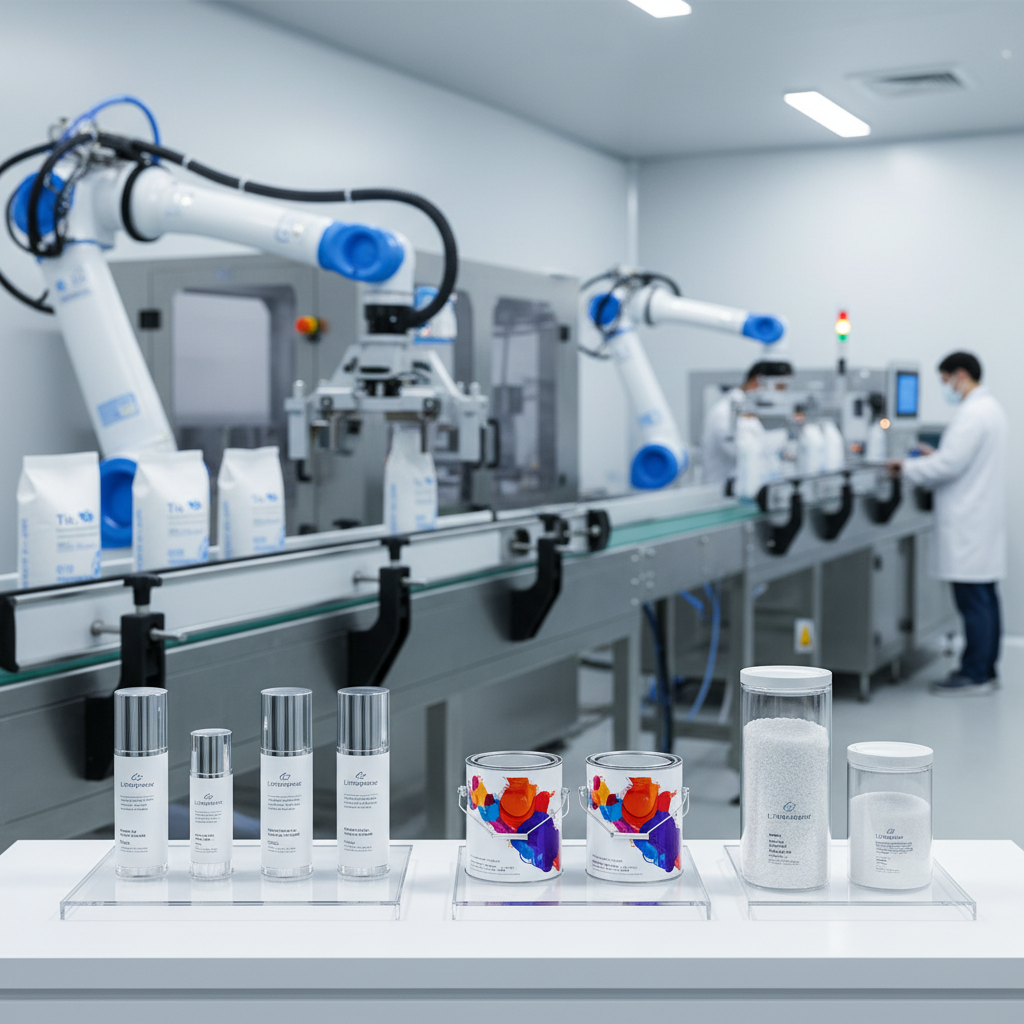


The industrial production of white pigments relies heavily on a sophisticated titanium dioxide manufacturing process to achieve the precise refractive index and particle size required for high-performance coatings. While the chemical formula TiO2 remains constant, the method of synthesis dictates whether the resulting pigment is the rutile or anatase crystalline form, which in turn defines its durability and opacity.
Selecting the right grade of TiO2 is not merely a matter of color, but a technical decision based on the desired weather resistance and scattering efficiency. From the sulfate process to the chloride route, each manufacturing pathway introduces different chemical characteristics that impact the final product's interaction with UV radiation and resin binders.
For professionals in the chemical raw materials and inorganic salt manufacturing sector, understanding these production nuances is critical for optimizing the performance of exterior wall coatings and industrial plastics. This analysis explores the technical intersection of manufacturing methods and the resulting material properties.

Technical Pathways of Titanium Dioxide Production

The titanium dioxide manufacturing process generally diverges into two primary chemical routes: the sulfate process and the chloride process. The sulfate method involves reacting ore with sulfuric acid to create a soluble titanyl sulfate, which is then hydrolyzed and calcined. This route is often preferred for producing anatase grades and specific specialty pigments due to its flexibility in controlling particle morphology.
Conversely, the chloride process utilizes titanium tetrachloride (TiCl4) as an intermediate, which is then oxidized with oxygen and chlorine gas. This method typically produces rutile TiO2 with higher purity and superior brightness. The choice between these pathways affects the pigment's overall chemical stability and its compatibility with various organic resins used in the coatings industry.
Hebei Caiqing New Material Technology Co., LTD leverages these industrial standards to provide a diverse range of products, including the CR-930 rutile series and BA01-01 anatase series, ensuring that the manufacturing route aligns with the specific technical requirements of the end application, such as cold resistance or dispersibility.
Core Attributes of Rutile vs Anatase TiO2
While both crystalline forms share the same chemical formula, their physical behavior under environmental stress differs significantly. Rutile TiO2 possesses a higher refractive index (approximately 2.76), providing the highest possible covering power among white pigments. Its dense crystal structure makes it inherently more stable when exposed to external elements.
Anatase TiO2, while possessing high whiteness, is more photocatalytically active. This makes it suitable for indoor applications or specific chemical processes but less ideal for exterior walls where UV-induced "chalking" must be avoided. The manufacturing process must precisely control the transition from anatase to rutile during calcination to ensure the desired stability.
Key technical indicators such as Oil Absorption (≤26 g/100g) and TiO2 content (≥98.0%) serve as benchmarks for quality. These parameters determine how the pigment integrates into a paint formulation, affecting the final viscosity and the uniformity of the coating layer.
Critical Application Scenarios in Modern Industry
Exterior wall coatings represent one of the most demanding environments for TiO2. In these scenarios, rutile grades are indispensable because they can withstand harsh atmospheric pollutants, including SO2 and H2S, and resist the alkaline leaching typically found in cement substrates. This ensures that the coating maintains its integrity for 10 to 15 years.
Beyond architecture, TiO2 finds extensive use in the rubber and tire industry, where it provides not only color but also reinforcement and UV protection. In the paper industry, its high opacity allows for thinner, brighter sheets. The dispersibility of the pigment is crucial here; poor dispersion leads to streaks and uneven color distribution.
Specialized coatings like fluorocarbon paints and textured real-stone paints rely on the extreme covering power of high-grade rutile TiO2. By reducing the amount of pigment needed per square meter, manufacturers can lower costs without sacrificing the aesthetic brightness or the physical protection of the underlying structure.
Evaluating Performance Metrics and Scattering Efficiency
The efficiency of a TiO2 pigment is measured by its ability to scatter light and cover a substrate. A higher refractive index directly correlates to a lower required concentration of pigment to achieve full opacity. This is where the distinction between manufacturing grades becomes a financial variable for the buyer.
When comparing standard white pigments against high-performance rutile grades, the difference in UV resistance and gloss retention is stark. The following metrics illustrate the relative performance advantages of specialized manufacturing processes in terms of opacity, weatherability, and stability.
titanium dioxide manufacturing process Performance Metrics
As indicated, the optimized manufacturing process for rutile grades significantly enhances UV absorption and light scattering. This allows for a reduction in total paint volume while extending the service life of the coating, effectively increasing the ROI for large-scale construction projects.
Procurement Considerations for Industrial Pigments
Purchasing TiO2 is not simply about sourcing a white powder; it is about matching the pigment's technical indicators to the application's failure points. For instance, a coating destined for a coastal environment requires a pigment with superior salt-spray resistance and chemical stability to prevent premature discoloration.
Buyers should evaluate the Sieve Residue (45mesh ≤0.1%) and PH levels (6.5-8.0) to ensure the pigment does not introduce clumps or destabilize the pH of the resin system. High residue levels can lead to surface defects in high-gloss finishes, compromising the aesthetic value of the project.
Lead times also play a critical role in supply chain management. With quantities ranging from small trial batches (1-25kg) to industrial scales (>25,000kg), established suppliers like Hebei Caiqing provide scalable lead times from 5 to negotiated days, ensuring production continuity for manufacturers.
Future Directions in Sustainable Pigment Synthesis
The industry is currently shifting toward more environmentally sustainable manufacturing processes. There is an increasing focus on reducing the acid waste produced during the sulfate process and improving the energy efficiency of chloride oxidation. These innovations are likely to reduce the overall carbon footprint of pigment production.
Advanced surface treatment technologies are also evolving. By coating TiO2 particles with inorganic layers like alumina or silica, manufacturers can further enhance the pigment's dispersibility and UV stability. This allows for the creation of "ultra-weatherable" grades that could potentially extend coating life beyond 20 years.
The integration of AI-driven process control in factories may lead to more consistent particle size distributions. Such precision could minimize the amount of raw material required to achieve maximum opacity, making the entire lifecycle of the pigment more resource-efficient.
Decision Framework for TiO2 Grade Selection
To maximize the performance of a final product, engineers must choose a TiO2 grade based on a matrix of environmental stress, required opacity, and budget. A mismatch—such as using anatase in an exterior wall paint—will lead to rapid degradation and costly rework.
The following table provides a comparison of common TiO2 applications and the corresponding technical requirements to guide procurement and formulation decisions.
| Application | Recommended Grade | Critical Factor | Expected Outcome |
|---|---|---|---|
| Exterior Wall Paint | Rutile (CR-930) | UV Resistance | 15+ Year Durability |
| Indoor Decorative Paint | Anatase (BA01-01) | High Whiteness | Bright Interior Finish |
| Industrial Tires | Rutile Grade | Dispersibility | UV-Protected Rubber |
| Specialty Plastics | Rutile Grade | Thermal Stability | No Yellowing at Heat |
| Paper Coating | Anatase/Rutile Mix | Opacity | High-Brightness Sheet |
| Ceramic Glazes | Specialty TiO2 | Heat Resistance | Stable Color After Firing |
By aligning the manufacturing grade with the specific use case, companies can optimize their raw material costs while ensuring the highest possible quality standards for their clients. For detailed technical specifications and customized services, interested parties can explore the resources available at www.cqtitaniumdioxide.com.
Frequently Asked Questions
Conclusion
The selection of a titanium dioxide manufacturing process is a pivotal decision that balances chemical purity, crystalline structure, and cost-efficiency. Whether utilizing the rutile CR-930 series for extreme weather durability or the anatase BA01-01 for interior brightness, the alignment of pigment properties with the application environment is the only way to ensure product longevity.
As the industry moves toward more sustainable synthesis and precise surface treatments, the role of high-quality TiO2 remains central to the coatings and plastics sectors. For organizations seeking a reliable supply of high-performance white pigments, visiting www.cqtitaniumdioxide.com provides access to detailed technical data and customized procurement solutions.